3D Surface Engagement
The spherical radius maintains tangential contact with contoured CAD surfaces during multi-axis motion.
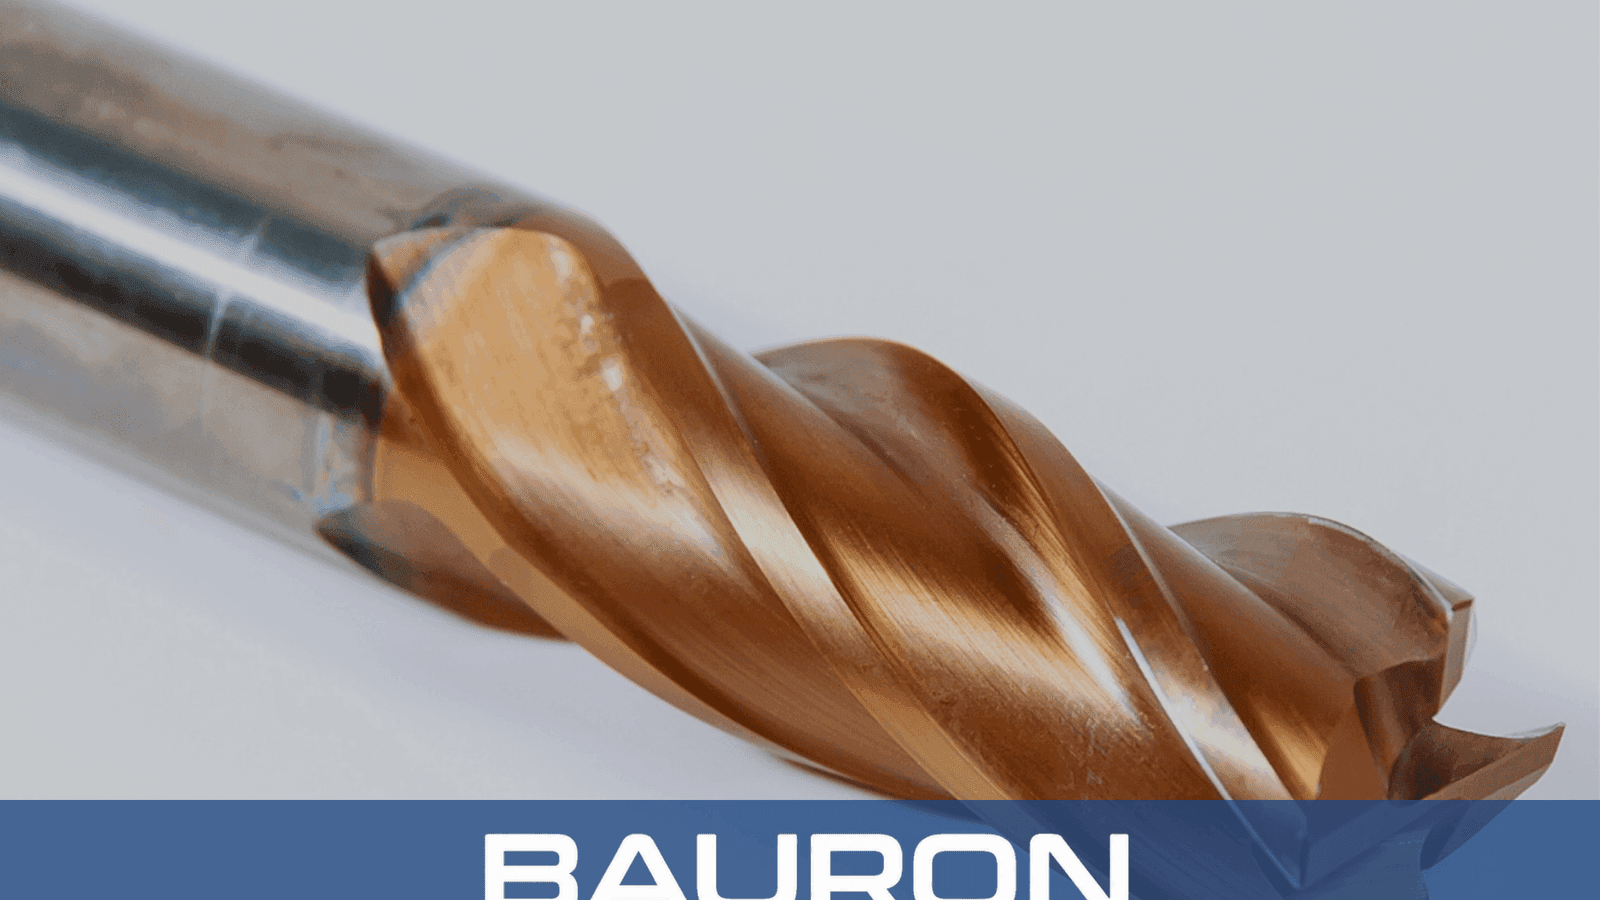
A ball nose end mill, also called a spherical end mill or ball nose cutter, has a rounded cutting nose where the flutes converge at the center of the tool radius. The hemispherical profile machines continuous 3D contours without leaving the sharp steps associated with a square end.
The spherical radius maintains tangential contact with contoured CAD surfaces during multi-axis motion.
Center-cutting flutes support direct plunging, ramping, and 3D profile carving.
Controlled stepover spacing leaves small surface scallops that can be polished.
The rounded geometry distributes cutting forces across the radius and reduces localized edge loading.
The spherical profile produces smooth contoured finishes and can reduce hand polishing.
Hemispherical geometry distributes cutting forces during complex multi-axis toolpaths.
Supports ramping, helical plunging, shallow-surface finishing, and continuous 5-axis profiling.
Solid carbide construction supports dimensional control during high-speed finishing cuts.
Free-cutting spherical geometries spread wear across the radius during continuous contouring.
| Specification | Range / Details |
|---|---|
| Diameter Range | 1/32" to 1"+; metric 0.5 mm to 25 mm+ available |
| Flute Count | 2 flutes for soft metals and aluminum; 4 flutes for hard steels and stainless steel |
| Radius Tolerance | ±0.0002" or ±0.005 mm |
| Shank Style | Straight cylindrical, reach-necked, or stub shank |
| Cutting Center | True center-cutting geometry |
| Operation Type | 3D surface finishing, profiling, and die sinking |
| Material / Coating | Best For | Key Advantage |
|---|---|---|
| Micro-Grain Carbide | Hardened steels, stainless steel, and titanium. | Core stiffness helps limit deflection during high-speed 3D finishing. |
| nACo / AlTiN Coating | Hardened mold steels up to 65 HRC and dry milling. | Oxidation resistance protects the ball nose tip from thermal friction. |
| DLC / ZrN Coating | Aluminum, copper, and non-ferrous alloys. | Low friction helps prevent material welding on the center flutes. |
Micro-grain carbide provides stiffness for 3D finishing, nACo or AlTiN supports hardened steels and dry milling, and DLC or ZrN helps control material adhesion in non-ferrous alloys.
Maintain tool-vector engagement while contouring complex 3D surfaces.
Run high-RPM die-sinking passes for injection-mold cavities.
Use live tooling to radius medical implants and small turned features.
Machines cavities, core inserts, and parting lines for injection molds and stamping dies.
Finishes 3D aerodynamic geometries on turbine blades and impellers.
Finishes internal floor radii, corner fillets, and stress-relieving pockets on aerospace structures.
Sculpts freeform contours in plastics, composite tooling board, and non-ferrous metals.
The rotational radius at the exact tip is zero, so surface speed at that point is also zero. On shallow surfaces, a 5-axis machine can tilt the tool 15° to 30° so cutting occurs along the higher-velocity outer radius.
Use 2 flutes for aluminum, copper, and plastics where open flute valleys aid chip evacuation. Use 4 flutes for steels, stainless steel, and titanium where a stronger core and more cutting edges support higher table feed rates.
Scallop height is the ridge of unmachined material left between adjacent finishing passes. Smaller stepovers and larger tool radii produce lower scallops and smoother surfaces.
A ball nose end mill has a full hemispherical tip with a radius equal to half its diameter for 3D sculpting. A bull nose tool has a flat bottom with rounded outer corners for pocket floors and floor-to-wall radii.
Bauron can engineer custom neck reach ratios, ball-radius tolerances, helix angles, and coatings for application-specific 3D CAD/CAM requirements.
Bauron provides design and engineering support for custom reach ratios, ball-radius tolerances, helix angles, and application-specific coatings. Share 3D models and machining requirements for technical review.
Talk to Engineering