High-Speed Shearing
Angled flutes shear material across the active chamfer margin at non-zero cutting speed.
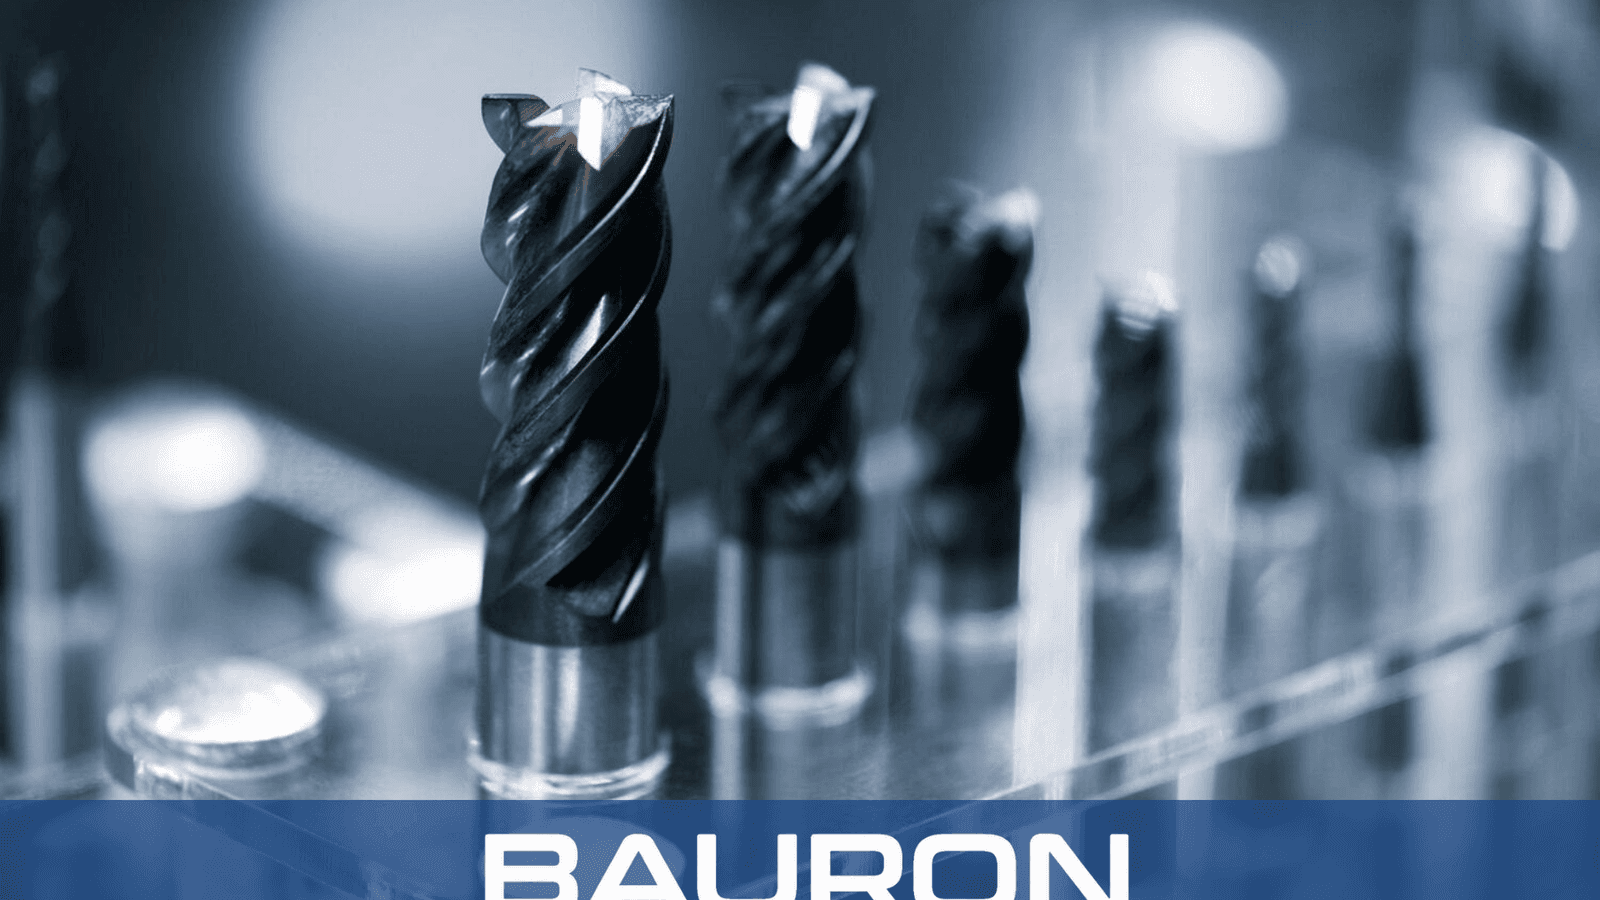
Tipped-off chamfer cutters are form-milling tools with a flat, truncated tip instead of a sharp point. Removing the zero-surface-speed point creates a thicker core that supports higher feed rates and heavier axial engagement than a pointed design.
Angled flutes shear material across the active chamfer margin at non-zero cutting speed.
The flat tip creates a thick web that resists chipping, snapping, and chatter under side loads.
The cutter follows straight or contoured edges to apply 30°, 45°, or 60° chamfers.
Higher flute counts support increased table feed rates in stable CNC milling setups.
The truncated flat tip removes the delicate point and improves resistance to tip chipping.
Increased core rigidity supports higher feed rates than pointed chamfer tools in suitable applications.
Cutting occurs away from the zero-surface-speed center point, supporting cleaner shearing.
Available with 4, 6, or 8 flutes for stable, high-feed machining setups.
Free-cutting geometry can reduce spindle torque during heavy edge-beveling passes.
| Specification | Range / Details |
|---|---|
| Diameter Range | 1/4" to 1"+; metric 6 mm to 25 mm+ available |
| End Style | Truncated or flat tipped-off profile |
| Chamfer Angles | 30°, 45°, and 60°; corresponding standard included angles of 60°, 90°, and 120° |
| Flute Count | 3, 4, 6, or 8 flutes |
| Shank Type | Straight cylindrical or Weldon shank |
| Operation Type | High-feed edge deburring, structural beveling, and countersinking |
| Material / Coating | Best For | Key Advantage |
|---|---|---|
| Solid Carbide | Hardened steels, stainless steel, and cast iron. | Core stiffness limits tool flex during heavy beveling. |
| TiAlN / AlTiN Coating | Tough alloy steels, titanium, and dry milling. | Thermal stability protects the cutting lips during continuous passes. |
| nACo / DLC Coating | Aluminum, brass, and non-ferrous metals. | Low friction helps prevent material welding and built-up edge. |
Solid carbide provides core stiffness, TiAlN or AlTiN supports tough alloys and dry machining, and nACo or DLC helps manage built-up edge in non-ferrous metals.
Run automated deburring and beveling cycles.
Perform structural beveling passes on large machinery frames.
Use live-tool turrets to chamfer turned shoulders and large outside diameters.
Applies structural bevels and weld-preparation angles along plate edges.
Cleans sharp milled shoulders, keyways, and large-bore openings in CNC production.
Prepares bolt holes and counterbores with the rigid flat-tip geometry.
Uses flat-tip clearance near pocket floors while beveling vertical sidewalls.
A pointed cutter can enter small holes and narrow V-bottoms. A tipped-off cutter removes the fragile point, producing a stronger tool for higher feed rates and heavier cuts on open edges.
Account for the flat-tip diameter and offset the toolpath downward so the workpiece edge contacts the middle of the angled flute while the flat tip and shank remain clear.
A pointed tool reaches zero cutting speed at its tip. Truncating the tip keeps the active cutting area at a non-zero radius, where the higher surface speed supports cleaner shearing.
Only when the pre-drilled hole is larger than the cutter's flat-tip diameter. A pointed chamfer cutter is needed when the hole is smaller than that tip flat.
Bauron can engineer specific flat-tip diameters, chamfer angles, extended neck lengths, flute counts, and application-specific coatings from production drawings.
Bauron provides design and engineering support for custom flat-tip diameters, chamfer angles, neck lengths, flute counts, and application-specific coatings. Share production drawings for technical review.
Talk to Engineering