Centering Entry
The 3-to-5-thread chamfer guides the tap into the pre-drilled pilot hole.
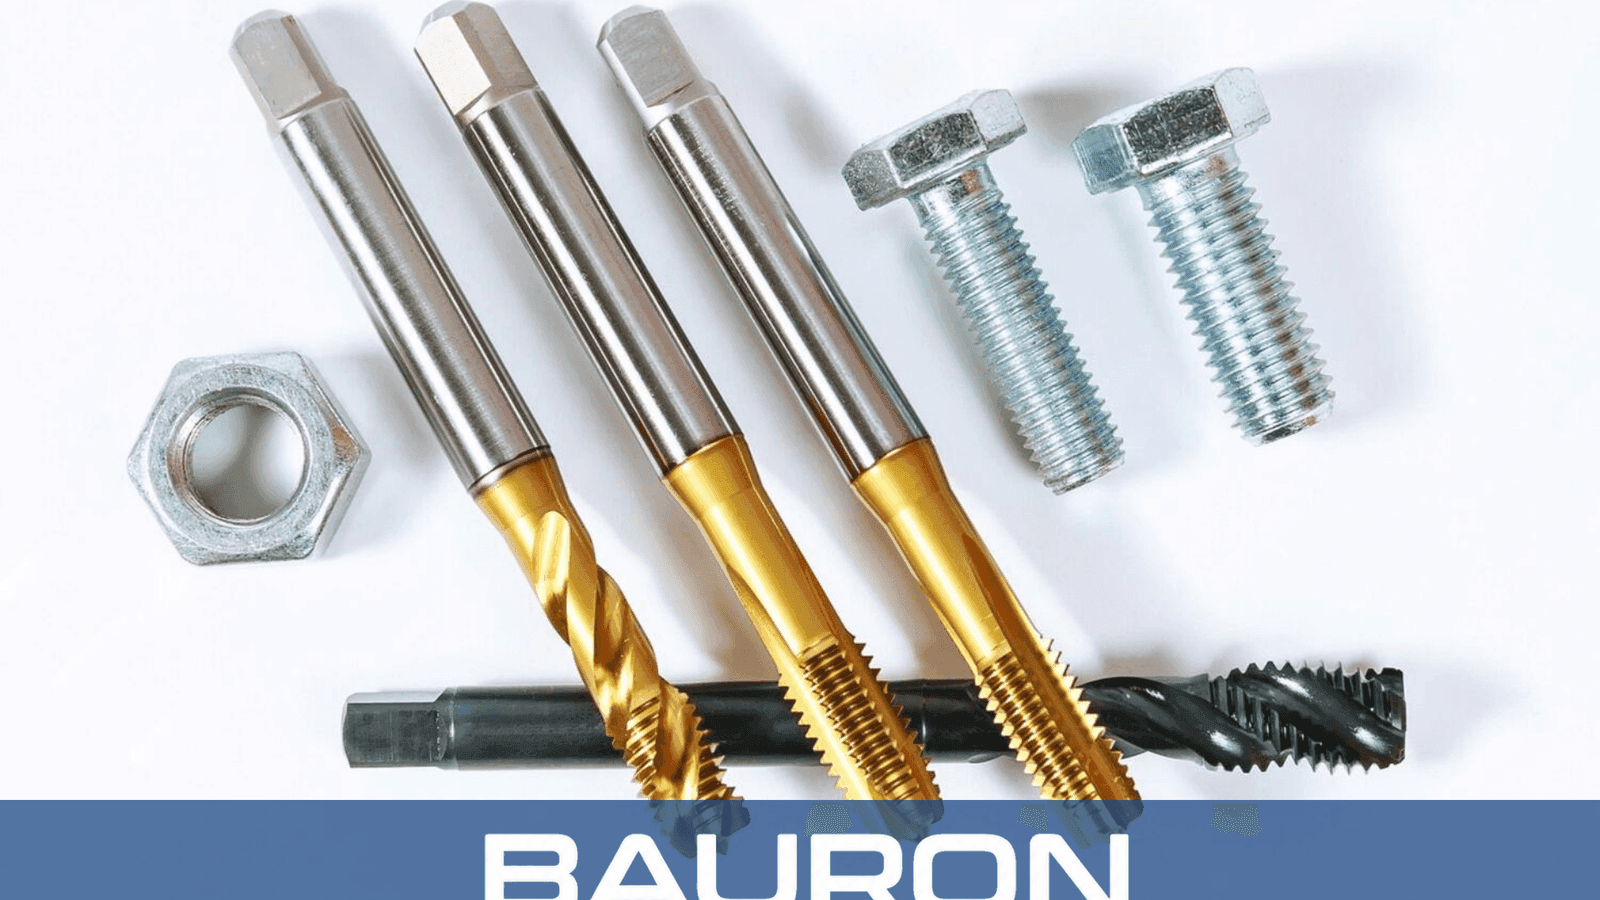
Plug taps are general-purpose internal thread-cutting tools with a medium chamfer across the first 3 to 5 threads. This geometry balances starting guidance with thread reach, allowing one tap to thread many through-holes or prepare blind holes for a bottoming pass.
The 3-to-5-thread chamfer guides the tap into the pre-drilled pilot hole.
Several lead teeth share the cut to keep starting torque manageable in manual or machine tapping.
Full-profile teeth behind the chamfer complete the internal thread as the tool advances.
Straight, spiral-point, or spiral-flute geometries control chips in ways suited to different hole and material conditions.
The medium chamfer supports through-hole threading and initial blind-hole passes.
The lead distributes cutting stress over several teeth without the length of a taper-tap chamfer.
Ground thread geometry supports clean pitch lines when matched to the required fit and operating conditions.
Straight-flute, spiral-point, and spiral-flute styles provide different chip-control behavior.
Plug taps can be supplied in matching size ranges or combined with taper and bottoming taps.
| Specification | Range / Details |
|---|---|
| Diameter Range | #0 to 2"+; metric M1.6 to M50+ available |
| Chamfer Profile | 3 to 5 tapered lead threads; medium lead |
| Thread Forms | UNC, UNF, metric, NPT, and custom pitches |
| Flute Geometry | Straight flute, spiral point, or spiral flute |
| Shank Type | Standard square drive or straight cylindrical |
| Tolerance | GH and H-class precision options |
| Material / Coating | Best For | Key Advantage |
|---|---|---|
| HSS (High-Speed Steel) | Mild steel, aluminum, brass, and plastics. | Impact toughness supports dependable general-purpose tapping. |
| Cobalt (HSS-Co) | Stainless steel, titanium, and high-temperature alloys. | Improved hot hardness helps retain cutting edges under elevated temperatures. |
| TiN / TiAlN Coating | Higher-speed automated CNC production. | Added surface hardness and lower friction can reduce thread-edge galling. |
HSS offers toughness for general tapping, cobalt improves hot hardness in demanding alloys, and TiN or TiAlN coatings can lower friction in automated production.
Run controlled rigid-tapping cycles for through-hole and blind-hole thread starting.
Hold plug taps in turrets or tailstock tooling for axial internal threads.
Use suitable tap holders for aligned workshop thread cutting.
Provide direct control for maintenance, assembly, and low-volume threading.
Cuts internal threads through open-ended components in one controlled operation.
Handles routine internal threading in production and maintenance settings.
Establishes most of the thread before a bottoming tap finishes closer to the cavity floor.
Restores or cleans existing internal threads when the correct size and fit are selected.
Chamfer length is the main difference. Taper taps typically have 7 to 10 lead threads, plug taps 3 to 5, and bottoming taps 1 to 2 for cutting closer to a blind-hole floor.
A plug tap can thread a blind hole but leaves several incomplete threads at the base because of its chamfer. Use a bottoming tap afterward if the design requires full-form threads closer to the floor.
A size set supports common thread dimensions, while a taper-plug-bottoming set provides different chamfer lengths for starting, general cutting, and blind-hole finishing.
Spiral-point geometry pushes chips forward and is well suited to machine tapping through-holes. Straight flutes are often used for short-chipping materials or controlled manual work.
Application-specific options can include non-standard pitches, extended shanks, coolant-through channels, flute geometries, and coatings.
Bauron provides design and engineering support for custom thread dimensions, flute geometries, shank configurations, coolant delivery, and application-specific coatings. Share the thread and process requirements for technical review.
Talk to Engineering